Laser cutting efficiency is not simply a matter of increasing feed rate. A fast cut can still waste time if parts need rework, sheets are poorly nested, or operators wait for material. In 2026, manufacturers looking at how to improve production efficiency with laser cutting should assess the whole workflow, from job preparation to finished-part handling. Small delays add up.
Start with measurable details: cutting time per part, material utilization, setup time, scrap rate, and machine downtime. Compare jobs using the same material thickness and grade; otherwise, the results may mislead. Better nesting can reduce offcuts, while consistent focus settings and clean optics help maintain cut quality. Nozzle condition, assist-gas pressure, and material flatness also matter. A rough edge may point to a process issue, not a need to raise power.
Automation, scheduling software, and real-time monitoring can shorten idle periods, but they are not instant fixes. Their value depends on reliable data, trained operators, and equipment that suits the workload. A simple trial on one recurring part may reveal more than a major system change. Even then, results can vary between shifts. That deserves attention. This guide explores practical ways to improve throughput without treating speed as the only goal. It also considers the trade-offs: higher output should not come at the expense of cut consistency, safe operation, or predictable delivery. When evaluating any adjustment, document the material, settings, and outcome so the team can repeat what works—and revisit what does not.
Assess Current Laser Cutting Capacity and Production Bottlenecks
Before changing schedules or adding shifts, measure what the laser cell actually produces. Rated cutting speed is only a starting point. Track completed parts per shift, machine-on time, setup duration, and sheet utilization for at least two representative weeks. Include different materials and thicknesses. Otherwise, a steel-heavy week may hide problems that appear on thin aluminum jobs. That happens.
Map each job from drawing release to packed parts, and record waiting time at every handoff. Compare laser runtime with loading, unloading, nozzle changes, focus checks, and quality inspection. Watch the floor, not just the dashboard. A machine can show high utilization while producing little if it waits for approved files or material. Check scrap, rework, and queue length alongside cycle time. These figures can reveal constraints beyond the cutting head, such as nesting delays, inconsistent blanks, or slow deburring.
Rank the losses by minutes per shift, then test one change at a time. For example, stage the next sheet near the cell and prepare verified programs before the current job ends. Keep a simple before-and-after log. Do not assume automation is the answer. Sometimes the bottleneck is a late drawing revision or one operator covering several stations. Capacity estimates will remain imperfect; production mixes change, and small samples can mislead. Review them monthly.
How to Boost Laser Cutting Production Efficiency in 2026?
Assess Current Laser Cutting Capacity and Production Bottlenecks
Illustrative audit of a 40-hour weekly production schedule: the example shows 12 hours of lost time across setup, material handling, maintenance, programming, and quality checks. Use measured shop-floor data to identify the largest losses and prioritize improvements.
Optimize Material Preparation, Nesting, and Job Scheduling
How to Boost Laser Cutting Production Efficiency in 2026?
Efficient cutting starts with reliable material preparation. Check sheet thickness, flatness, surface condition, and protective film before loading. A slightly bowed sheet can disrupt focus and create inconsistent edges. Keep material labels visible, and separate remnants by grade and thickness. Small checks matter. Record recurring defects, too; a quick note about burrs or warped corners can prevent the same delay next shift.
Nesting software can reduce scrap, but a tight layout is not automatically a good one. Respect grain direction when the part requires it, allow suitable spacing for heat, and group jobs with matching material and thickness. Test a sample part before releasing a new layout. Scheduling should account for setup changes, material availability, and promised delivery times—not just total cutting minutes. Running similar jobs together often saves nozzle and gas changes, while a clearly marked urgent order can still take priority. We still get this wrong sometimes: a full table looks productive, even when unloading becomes the bottleneck. Track both machine time and handling time, then adjust the plan using actual shift data.
How to Boost Laser Cutting Production Efficiency in 2026? — Optimize Material Preparation, Nesting, and Job Scheduling
Illustrative before-and-after operating metrics for a single laser-cutting cell running one 8-hour shift. Results depend on material mix, machine capacity, staffing, and order complexity.
| Improvement Area |
Metric |
Current Baseline |
Optimized Operating Target |
Change |
Practical Action |
| Material preparation |
Average material staging time per job |
18 min |
10 min |
8 min less |
Stage the correct sheet, thickness, and grade near the machine before the scheduled job starts. |
| Material preparation |
First-sheet start delay after job release |
35 min |
20 min |
15 min less |
Use a pre-cut checklist for material identification, sheet condition, program revision, and required tooling. |
| Nesting |
Material utilization per sheet |
82% |
90% |
+8 percentage points |
Group compatible parts by material, thickness, and due date; review grain direction and minimum spacing before release. |
| Nesting |
Reusable remnant use as a share of sheet-material input |
6% |
14% |
+8 percentage points |
Label usable remnants with material, thickness, dimensions, and location, then check them before issuing a full sheet. |
| Job scheduling |
Average machine changeover between jobs |
38 min |
22 min |
16 min less |
Sequence jobs to reduce avoidable changes in material type and thickness, while protecting due dates. |
| Job scheduling |
Unplanned schedule changes per shift |
5.0 |
2.0 |
3 fewer per shift |
Set a daily schedule freeze window and route urgent work through a defined priority review. |
| Machine utilization |
Productive cutting time in an 8-hour shift |
6.4 hr |
7.2 hr |
+0.8 hr |
Track cutting, setup, waiting, and downtime separately to identify the largest sources of lost machine time. |
| Delivery performance |
Jobs completed by the committed shift or date |
86% |
95% |
+9 percentage points |
Schedule from realistic cycle-time estimates and confirm material availability before committing work. |
Measurement notes: Utilization is the part area used divided by the usable sheet area. Changeover time is the interval between completing one job and starting the next. Compare each metric over consistent shifts and product mixes; targets are planning examples, not guaranteed results.
Tune Cutting Parameters for Quality, Speed, and Material Type
How to Boost Laser Cutting Production Efficiency in 2026?
A faster feed rate is useful only when the edge stays within specification. Tune power, speed, focus position, and assist-gas pressure as a group; changing one setting can shift the others. Euro Inox technical property tables put 304 stainless steel’s thermal conductivity near 15 W/m·K at room temperature. Heat therefore spreads differently than it does in many carbon steels, so copying a recipe between materials can produce dross, a rough edge, or incomplete cuts. Start with the material supplier’s thickness-specific range, then make small test cuts. Inspect the underside for burrs and the top edge for discoloration. Small details matter.
Use ISO 9013:2017 to assess thermal-cut quality through measures such as perpendicularity tolerance and surface profile, rather than judging speed alone. Record the settings and results for each material and thickness. If the cut is clean but slow, increase speed in measured steps; if the edge degrades, check focus and gas delivery before adding power. A practical trial can still mislead: a fresh nozzle or different sheet batch may change results. Track these variables, too. A short test grid often reveals a stable production window more clearly than repeated operator adjustments.
Integrate Automation to Reduce Handling and Machine Downtime
How to Boost Laser Cutting Production Efficiency in 2026?
Integrate Automation to Reduce Handling and Machine Downtime
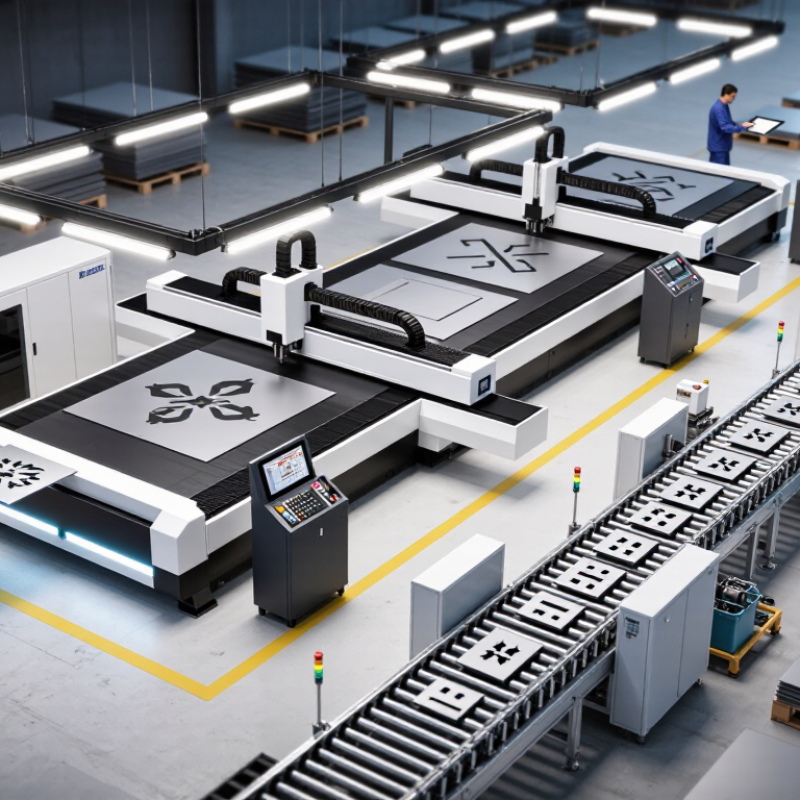
A laser cutting cell can lose valuable production time between jobs, not only during cutting. Operators may spend minutes unloading sheets, sorting parts, and positioning the next material. Automated loading and unloading reduce these repeated handling steps and keep the machine supplied more consistently. That matters. When finished parts move directly to a sorting area, operators can focus on quality checks and upcoming jobs instead of waiting beside the machine.
Automation works best when it matches the shop’s actual workflow. A loading system needs reliable sheet alignment, clear material identification, and enough buffer space for finished parts. Sensors can flag misfeeds before they cause a longer interruption. Still, automation is not magic. A rushed changeover or poorly prepared job can slow the whole cell, and automated equipment also needs regular inspection. Track loading delays, idle minutes, and misfeeds for several weeks. Those figures help reveal whether the bottleneck is material handling, programming, or maintenance. Start with one repeatable workflow, then adjust based on real production data. The first setup may need a rethink.
Track Performance and Maintain Equipment for Consistent Output
A laser cutter’s uptime is not the whole story. Track unplanned stops, cycle time, sheet changes, scrap, and rework by shift. A five-minute nozzle change seems minor, yet repeated interruptions quietly reduce output. Small signals matter. Compare jobs using the same material thickness and cut geometry; otherwise, cycle-time comparisons can mislead. Record nozzle condition, lens cleaning, assist-gas pressure, and edge quality alongside machine hours.
The U.S. Department of Energy’s 2010 Operations & Maintenance Best Practices Guide estimates predictive maintenance can reduce costs by 8–12% compared with preventive maintenance, and 30–40% compared with reactive maintenance. These are broad industrial estimates, not promises for a laser cell. The 2022 report The True Cost of Downtime estimates that downtime represents 11% of revenue among Fortune Global 500 companies, or about $1.4 trillion annually. That figure is not laser-specific, but it shows why lost production deserves careful measurement.
Use alarms and maintenance logs to spot recurring patterns, such as cut-quality drift before a scheduled lens inspection. Set practical thresholds for cleaning and replacement, then review whether they actually reduce stoppages. Not every alert needs action. Operators should note when a fault appears, what changed, and how long recovery took. A log can still be incomplete, especially during busy shifts; review it with operators before treating its numbers as the full story.
Conclusion
Boosting laser cutting production efficiency in 2026 starts with understanding how the current operation performs. Reviewing machine capacity, order flow, idle time, and recurring bottlenecks helps identify where production slows down. Better material preparation, efficient nesting, and thoughtful job scheduling can reduce waste, avoid unnecessary changeovers, and keep work moving smoothly.
To improve results further, match cutting parameters to the material and desired finish, balancing speed with quality. Automation can reduce manual handling and downtime, while regular equipment maintenance supports consistent output. Tracking measures such as cycle time, material use, and machine availability makes it easier to spot problems and assess improvements. Together, these practices offer a practical approach to how to improve production efficiency with laser cutting while maintaining reliable quality and making better use of available resources.
 Datum Machine